

离心铸造技术
介绍
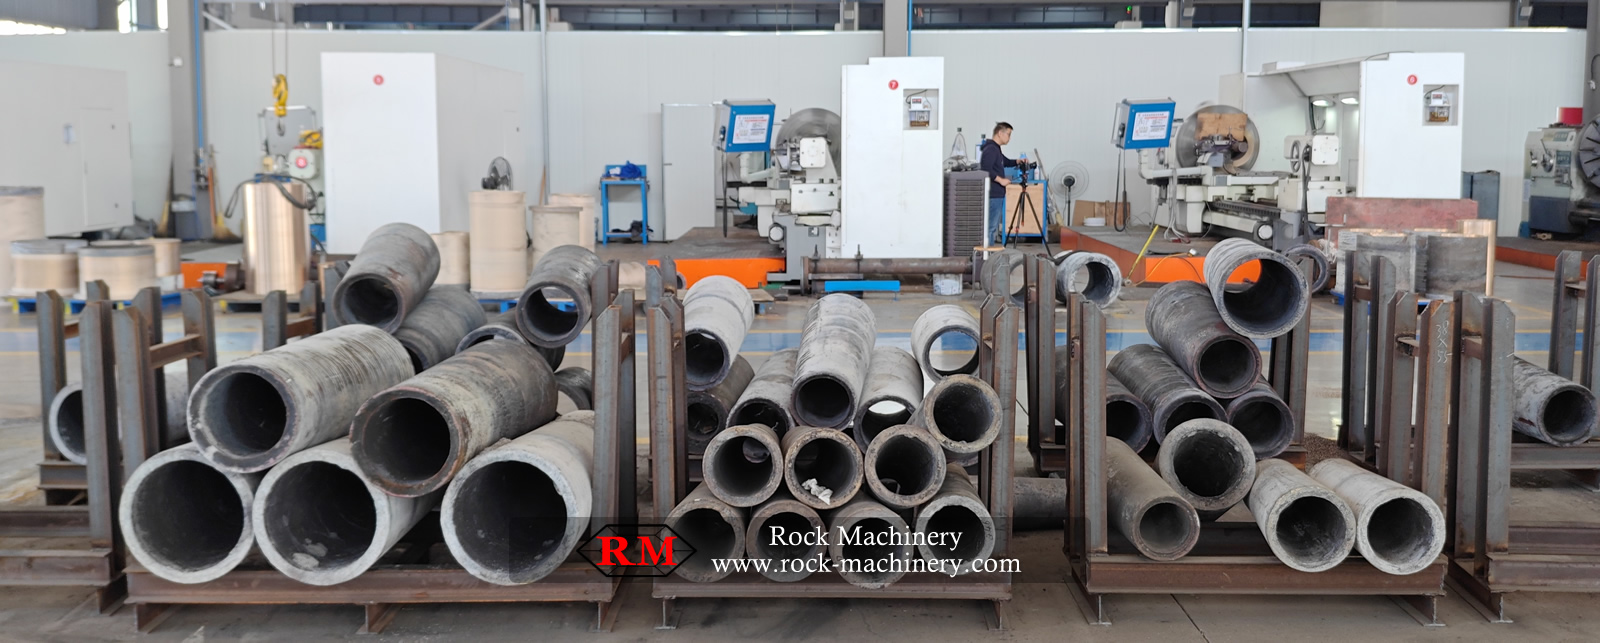
破碎机铜衬套减少圆锥和旋回破碎机中运动部件之间的摩擦。采用C93800、C93700及其他铜合金通过离心铸造生产。具有致密、无空隙的晶粒结构。
工艺概述
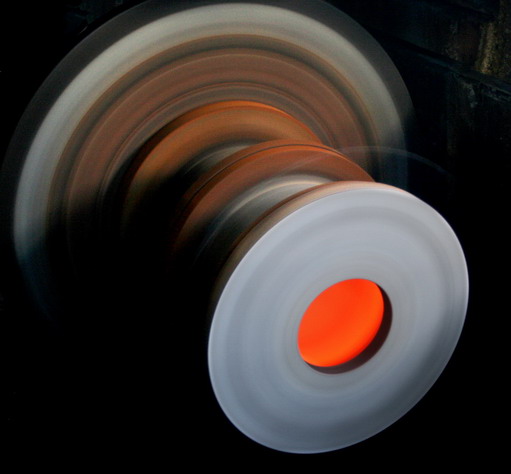
离心铸造通过高速旋转模具并注入熔融金属,离心力将金属向外推,使其在模腔内均匀分布,从而形成致密、均质且孔隙率极低的铸件。
离心铸造的步骤
1. Mold Preparation — The mold is made of a refractory material that can withstand high temperatures and has the desired inner shape of the bushing. It is lined with a release agent to facilitate easy removal of the casting.
2. Melting Process — The copper is melted in a furnace to reach a precise temperature suitable for casting.
3. Centrifugal Casting — The molten copper is poured into the rotating mold. The centrifugal force pushes the molten metal against the mold walls, forming a solid casting. The rotation speed determines the thickness and uniformity of the bushing.
4. Cooling and Solidification — The casting is allowed to cool inside the rotating mold. The controlled cooling rate promotes a fine-grained structure, improving the mechanical properties of the bushing.
5. Finishing — Once solidified, the casting is removed from the mold and undergoes finishing processes such as trimming, machining, and heat treatment to achieve the desired dimensions and properties.
Key Properties
高密度离心力使金属紧密贴合模壁,密度通常超过理论值的99.5%。
低孔隙率— 空气和气体夹杂物迁移至内表面,并在精加工过程中被切削掉。
细粒结构— 受控冷却速率产生均匀的微观结构。相比静态铸造件,具有更好的耐磨性和疲劳寿命。
高效适用于生产批次— 每周期可铸造多个衬套。模具成本低于永久模或压铸。
应用
离心铸造广泛应用于各行业生产破碎机铜衬套,包括:
- 采矿和采石
- 金属加工
- 水泥制造
- 混凝土生产
- 回收和废物管理
离心铸造生产出致密、均匀的衬套,具有细晶结构。适用于中大批量生产。批次间机械性能一致。衬套最大4吨,直径2.5米。
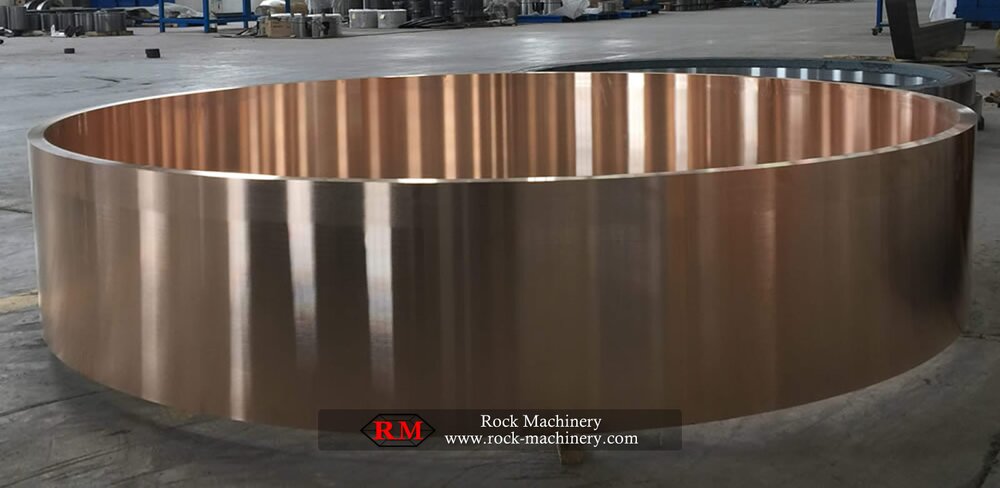
离心铸造能力:最大4吨(重量),2.5米(直径)。